Every Genious Engineering deployment follows a rigorous 5-stage closed-loop manufacturing and quality framework, ensuring zero-defect deliverables that integrate seamlessly into client production lines without costly field modifications.
Our engineering team conducts laser-level facility scans to map floor undulations, column spans, overhead crane clearances, and fire sprinkler envelopes. We generate complete 3D SolidWorks models and ANSYS structural stress simulations before any steel is processed.
| Workflow Deliverable | Engineering Protocol |
|---|---|
| Floor Leveling Survey | Optical & laser level mapping of shop-floor floor flatness and concrete anchor depths |
| 3D CAD Modeling | SolidWorks 3D General Arrangement (GA) drawings with exact component clearance checks |
| Structural FEA Validation | ANSYS stress simulation confirming deflection within L/200 limit under maximum payload |
| Customer Milestone | Formal client engineering sign-off on 3D drawings and bill of materials (BOM) |
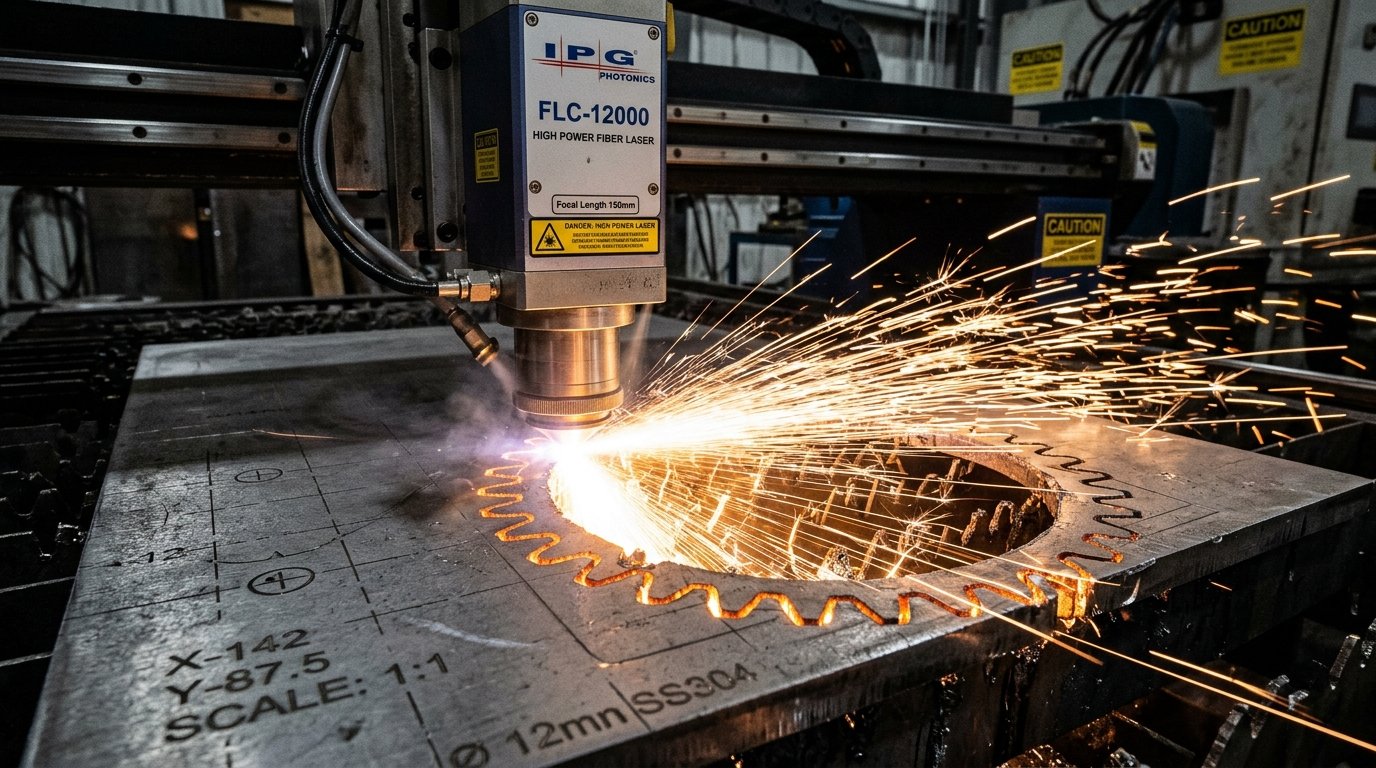
Processed on our 12.00 kW CNC fiber laser cutting center, sheet metal profiles are cut with ±0.03mm precision. Multi-axis CNC hydraulic press brakes with automatic crowning compensation bend structural channels with zero angular distortion over 4-meter spans.
| Workflow Deliverable | Engineering Protocol |
|---|---|
| Laser Cutting Precision | 12.00 kW CNC cutting of mild steel up to 25mm and stainless steel up to 16mm |
| Nesting Optimization | CAD/CAM algorithmic nesting achieving > 92% raw material utilization |
| Bending Repeatability | Multi-axis synchronized 250T CNC press brakes with ±0.05mm bend repeatability |
| Quality Inspection Gate | First-piece CMM dimensional verification before commencing production run |
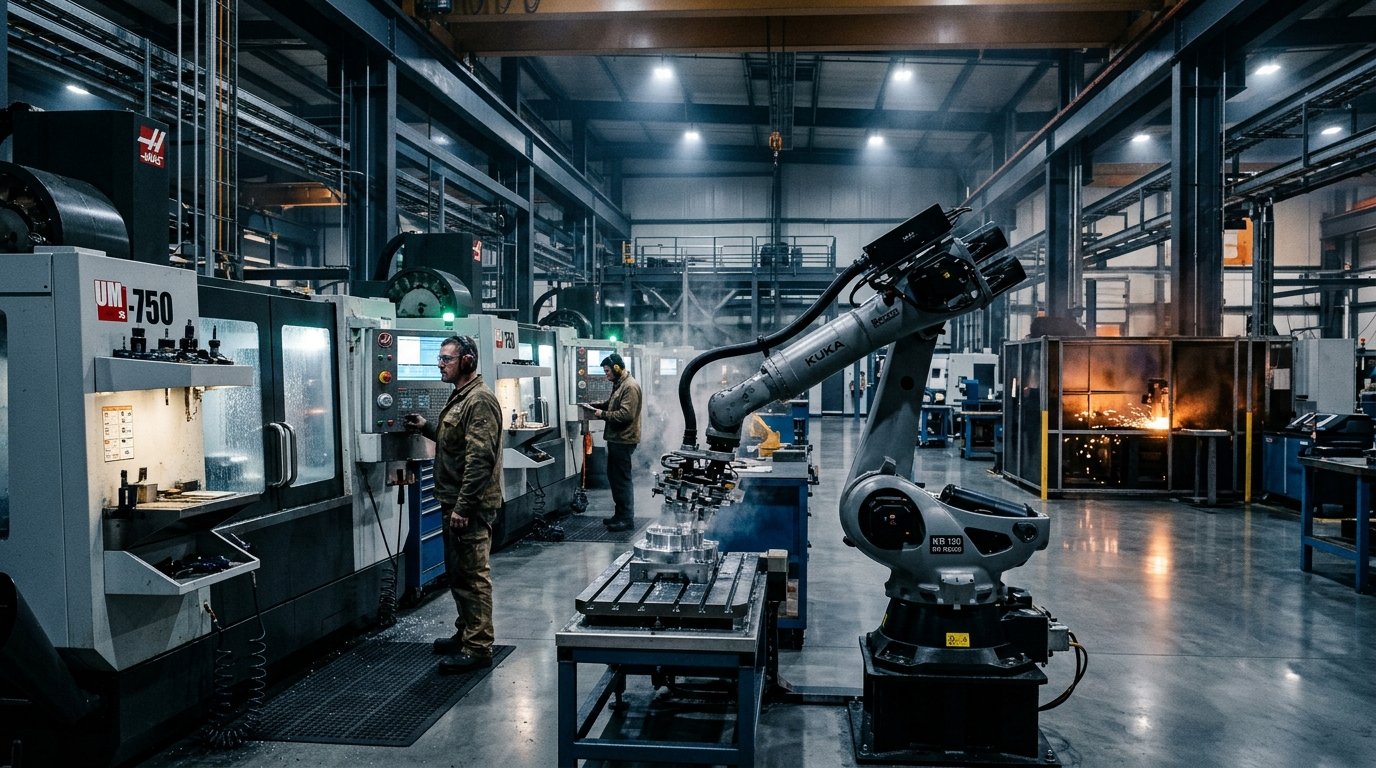
Heavy structural components, mezzanine baseplates, and stillages are fabricated by certified 6G welders and automated robotic MIG/TIG cells under AWS D1.1 structural welding standards. Custom clamping fixtures prevent thermal distortion during continuous weld passes.
| Workflow Deliverable | Engineering Protocol |
|---|---|
| Welding Standards | AWS D1.1 Structural Welding Code & certified 6G welder qualification records |
| Thermal Warpage Control | Heavy rigid jig clamping and sequenced back-step welding to eliminate twisting |
| Weld Non-Destructive Testing | Dye-penetrant (DPT) and ultrasonic flaw detection on critical load-bearing joints |
| Spatter Removal | Pneumatic descaling and post-weld mechanical grinding to ensure immaculate surface prep |
Every fabricated part undergoes hot chemical immersion across 7 distinct tanks: degreasing, water rinsing, derusting, water rinsing, zinc phosphating, water rinsing, and passivation. This creates an inert crystalline phosphate foundation followed by electrostatic powder deposition and 200°C oven curing.
| Workflow Deliverable | Engineering Protocol |
|---|---|
| Immersion Stages | Hot Alkaline Degrease → Rinse → Acid Pickling → Rinse → Zinc Phosphate → Rinse → Passivation |
| Powder Chemistry | Pure polyester & epoxy-polyester architectural powders from Asian Paints / AkzoNobel |
| Curing Profile | Conveyorized continuous oven with 200°C metal temperature soaking for 15 minutes |
| Corrosion Rating | 1,000-Hour salt spray endurance (ASTM B117) with 80–120 μm Dry Film Thickness |
Before leaving the plant, components undergo full trial pre-assembly and load testing. Our on-site rigging crew executes pan-India deployment with heavy laser alignment, precision anchor bolting, and formal client sign-off under strict Environmental Health & Safety (EHS) standards.
| Workflow Deliverable | Engineering Protocol |
|---|---|
| Factory Pre-Assembly | 100% bolt-hole alignment verification on test fixtures prior to packing |
| Packaging & Protection | Heavy bubble-wrap, corner edge protectors, and wooden pallets for transit integrity |
| On-Site Installation | Certified rigging engineers with Hilti anchoring, laser plumb leveling & torque audits |
| Handover Documentation | Comprehensive Load Test Certificates, ISO 9001:2015 sign-off & maintenance manuals |
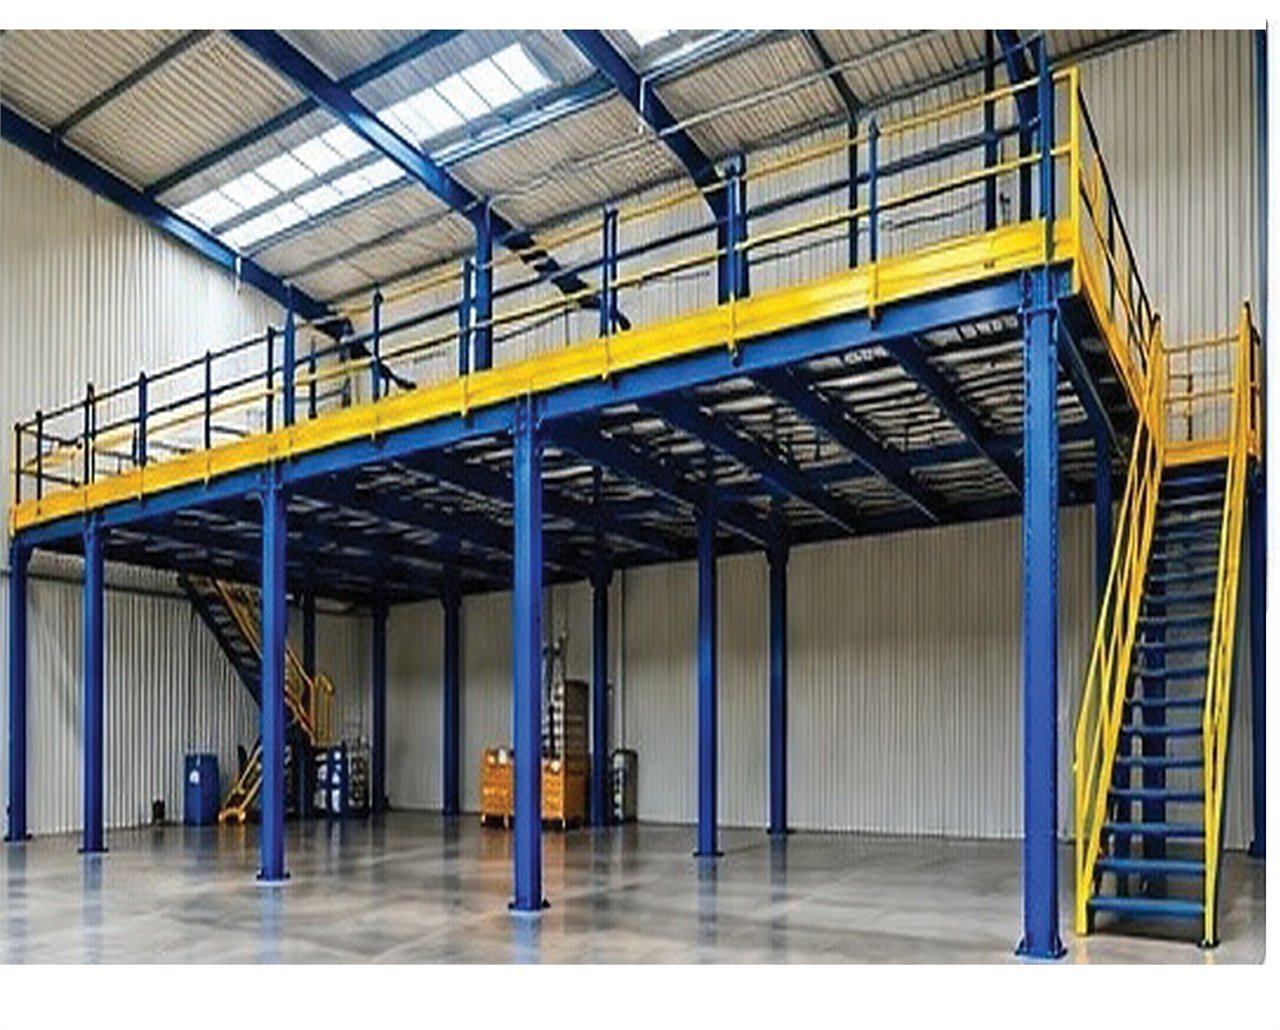
Our dedicated metrology lab ensures raw material certification, weld integrity, coating adhesion, and live beam deflection meet the highest international engineering codes.
Spectrometric chemical analysis and tensile yield testing verifying IS 2062 prime structural steel grades with batch heat numbers.
Digital Elcometer Dry Film Thickness (DFT) testing (80–120 μm) and cross-hatch tape adhesion tests confirming zero coating delamination.
Live hydraulic ram deflection testing up to 1.5x design working load to verify recovery without permanent beam or upright deformation.